Fibronexa
Explore our core engineering excellence powering global communication networks, data centers, and enterprise VoIP infrastructures.
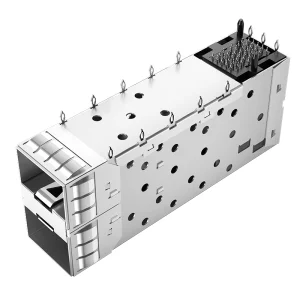
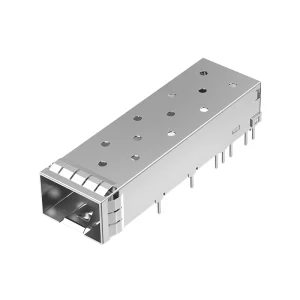
2007538-8 TE Compatible Through Hole 40P Press-Fit 2x1 EMI Shielded SFP+ Cage With Connector
View Details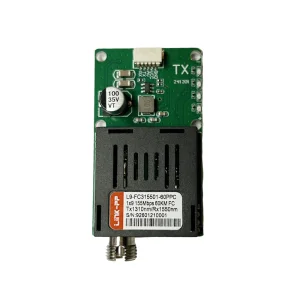
Single Mode 155M BiDi 1310nm-Tx/1550nm-Rx FC SMF 60km Air/Ground TTL 1x9 Optical Transceiver
View Details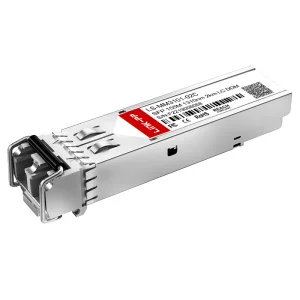
Moxa SFP-1FEMLC-T Compatible MMF Optical Module 100M Multimode 1310nm SFP Transceiver 2km
View DetailsAn authoritative industry analysis on how top-tier manufacturers and exporters are redefining enterprise telephony, network stability, and secure global connectivity.
Modern enterprises are rapidly shifting away from legacy analog systems toward cloud-native VoIP infrastructures. Procurement directors now demand hardware that guarantees ultra-low latency, seamless PBX integration, and robust Power over Ethernet (PoE) capabilities to reduce structural deployment costs.
China-based manufacturing hubs offer unmatched scalability, vertical integration of passive components, and rigorous automated testing protocols. This robust supply chain ecosystem ensures consistent batch quality, rapid prototype iterations, and competitive pricing for international importers.
Global compliance—including FCC, CE, RoHS, and ISO standards—is non-negotiable. Leading suppliers integrate regional telecommunication safety protocols, localized multi-language firmware support, and encrypted VoIP signaling to protect sensitive corporate communications.
Backed by over a decade of specialized R&D and manufacturing excellence in optical communication and networking hardware.
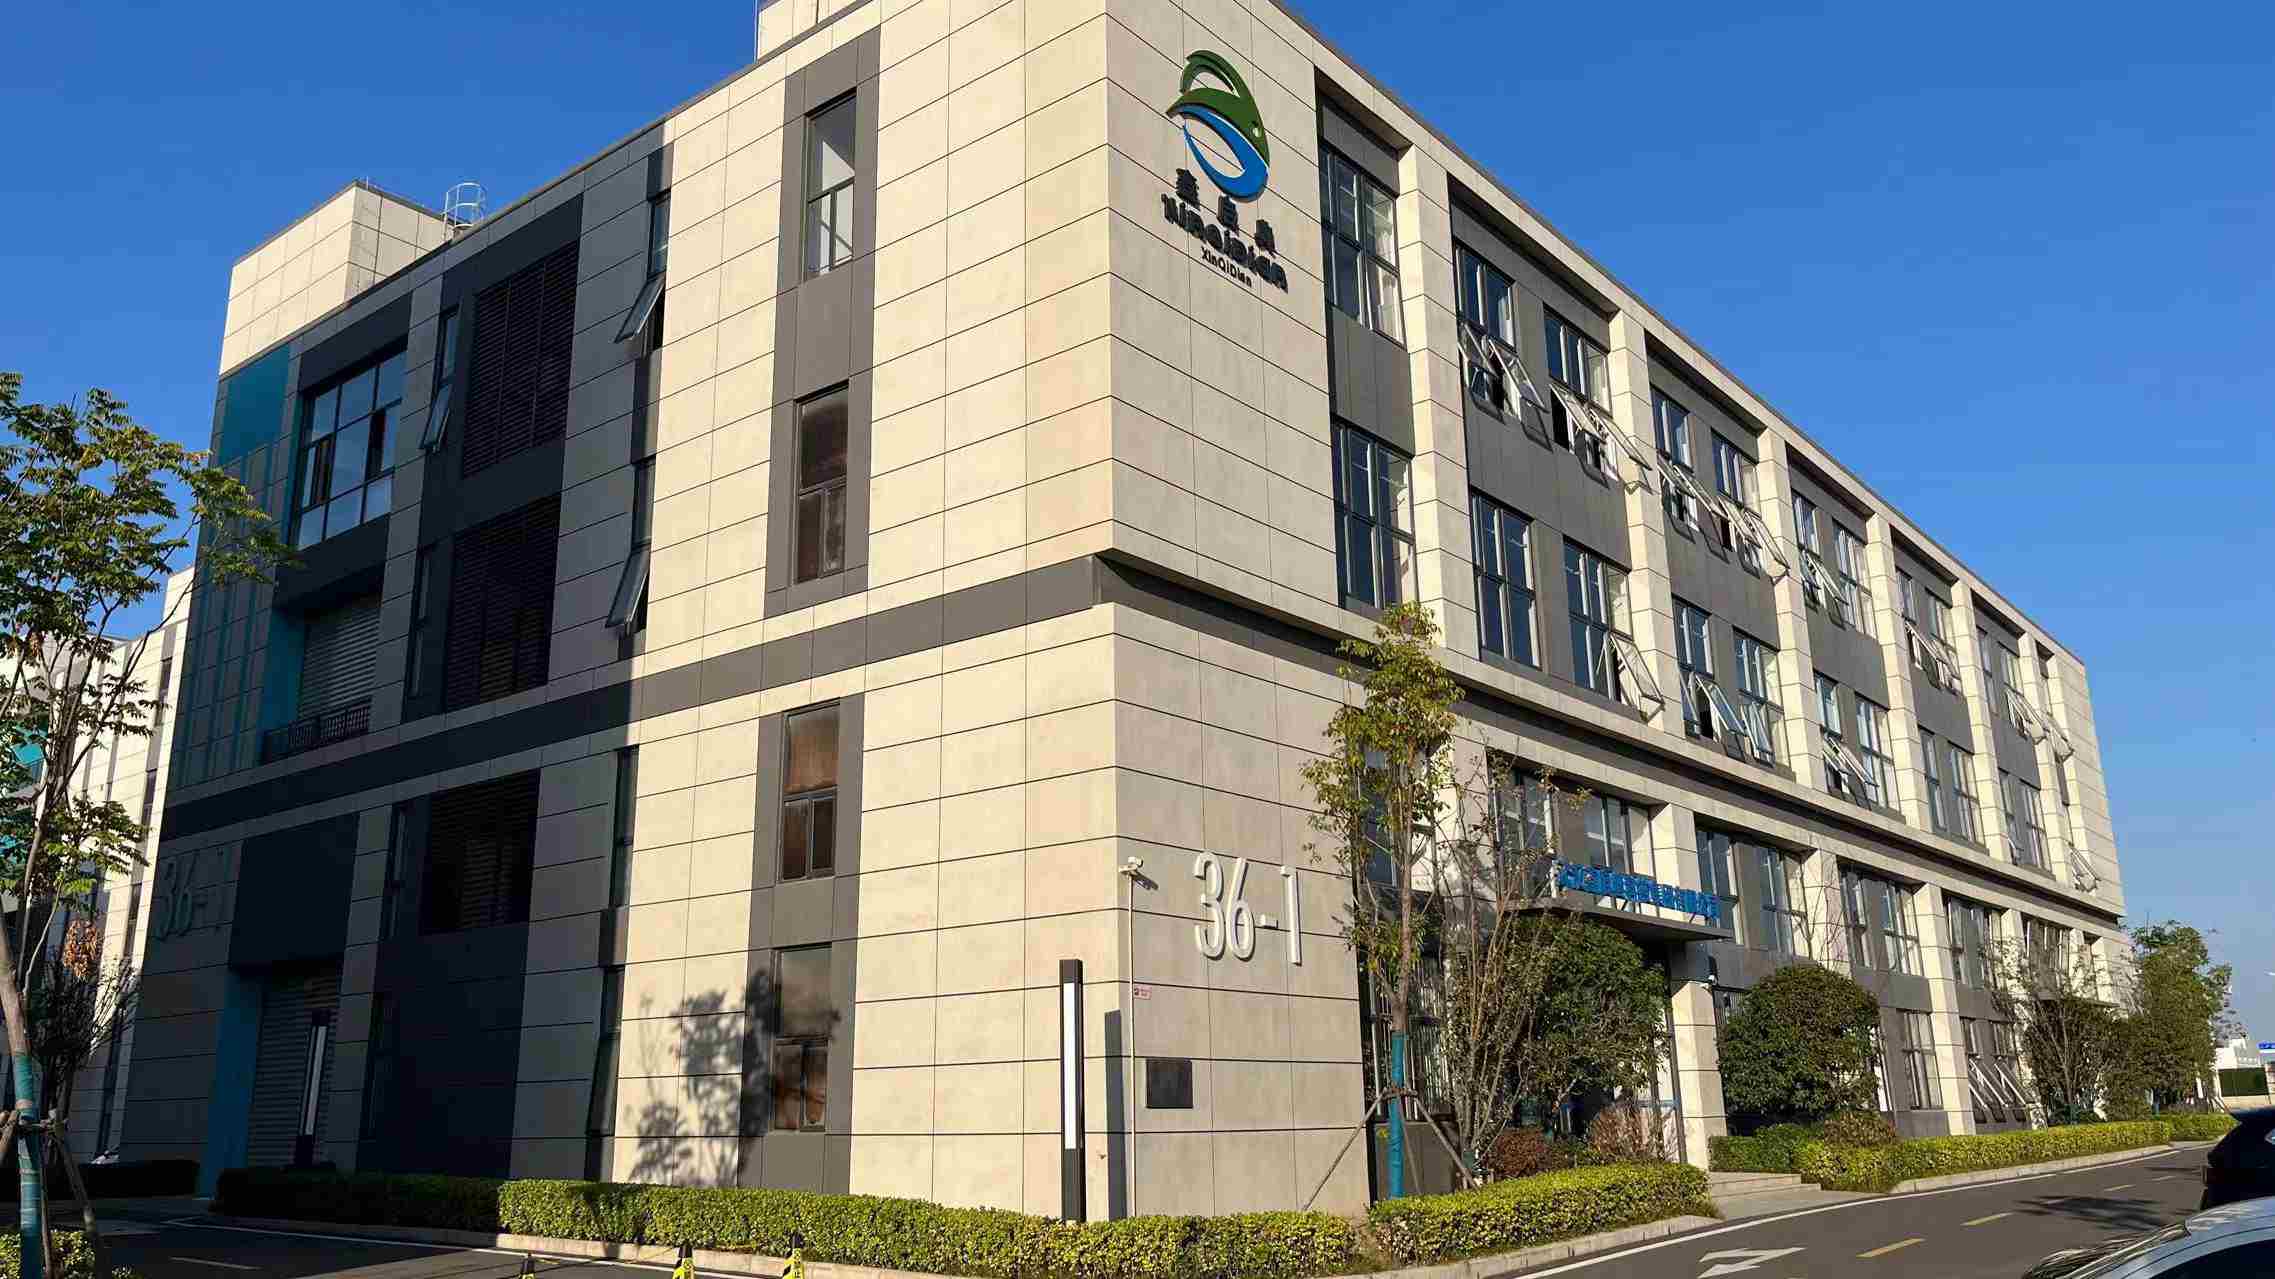
Fibronexa Communications Co., Ltd. (Fibronexa Optical Transceiver Manufacturer) was established in 2016, specializing in high-speed fiber optic communication solutions for global data center and telecom infrastructure markets. With a modern production facility covering approximately 320㎡, Fibronexa has built a stable and efficient manufacturing system supported by advanced automation and precision assembly processes.
The company generates an annual export revenue of around USD 12 million, with over 6 years of export experience and 10 years of accumulated industry expertise in optical communication technology. Fibronexa has developed strong global trade capabilities, serving customers across North America, Europe, Southeast Asia, and the Middle East.
Quality is strictly controlled through a combination of automated optical testing systems and manual inspection processes, including 100% performance testing and environmental stress screening. The quality assurance team consists of approximately 45 trained QC professionals, ensuring every product meets international standards for reliability and performance.
Fibronexa maintains a robust supply chain network with more than 1,200 strategic upstream and downstream partners, enabling stable component sourcing and fast production scalability. The company primarily serves telecom operators, data center integrators, enterprise network solution providers, and OEM/ODM customers worldwide.
Driven by strong engineering capabilities, Fibronexa operates with a R&D team of around 85 engineers, focusing on high-speed optical modules, including 10G, 25G, 100G, 400G, and emerging 800G solutions. The company launched approximately 120 new products in the past year, with flexible customization options available for wavelength, distance, packaging, and protocol compatibility.
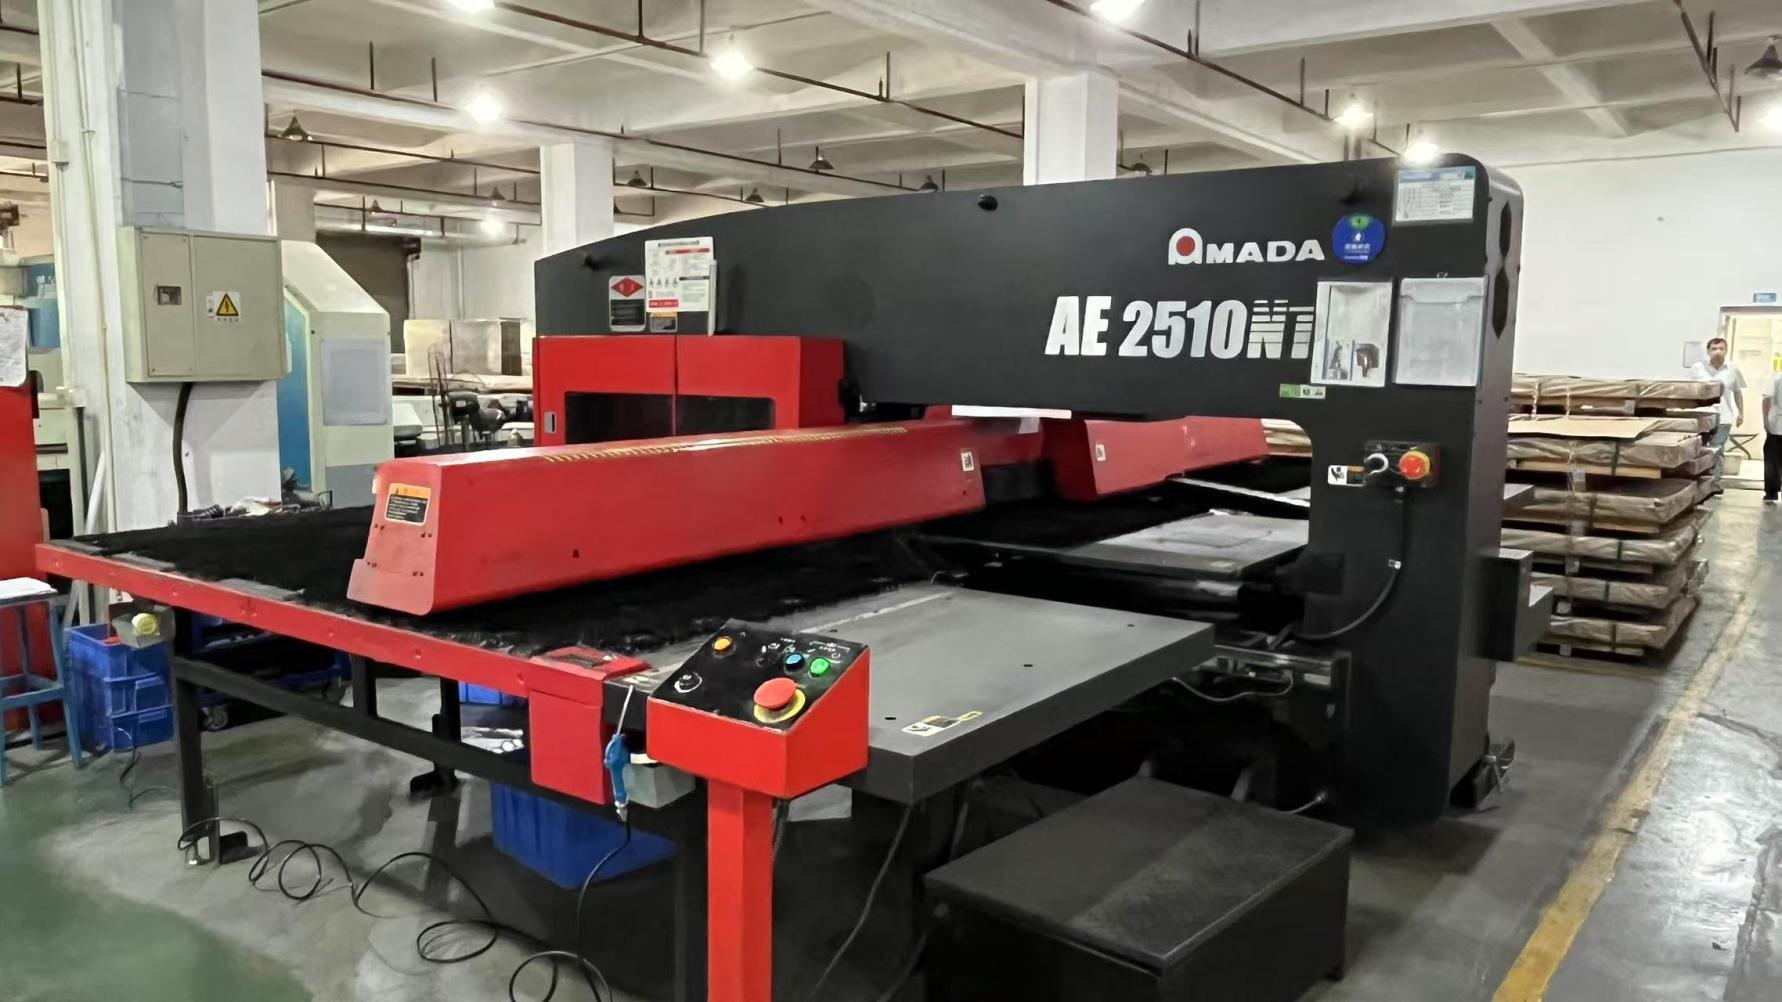
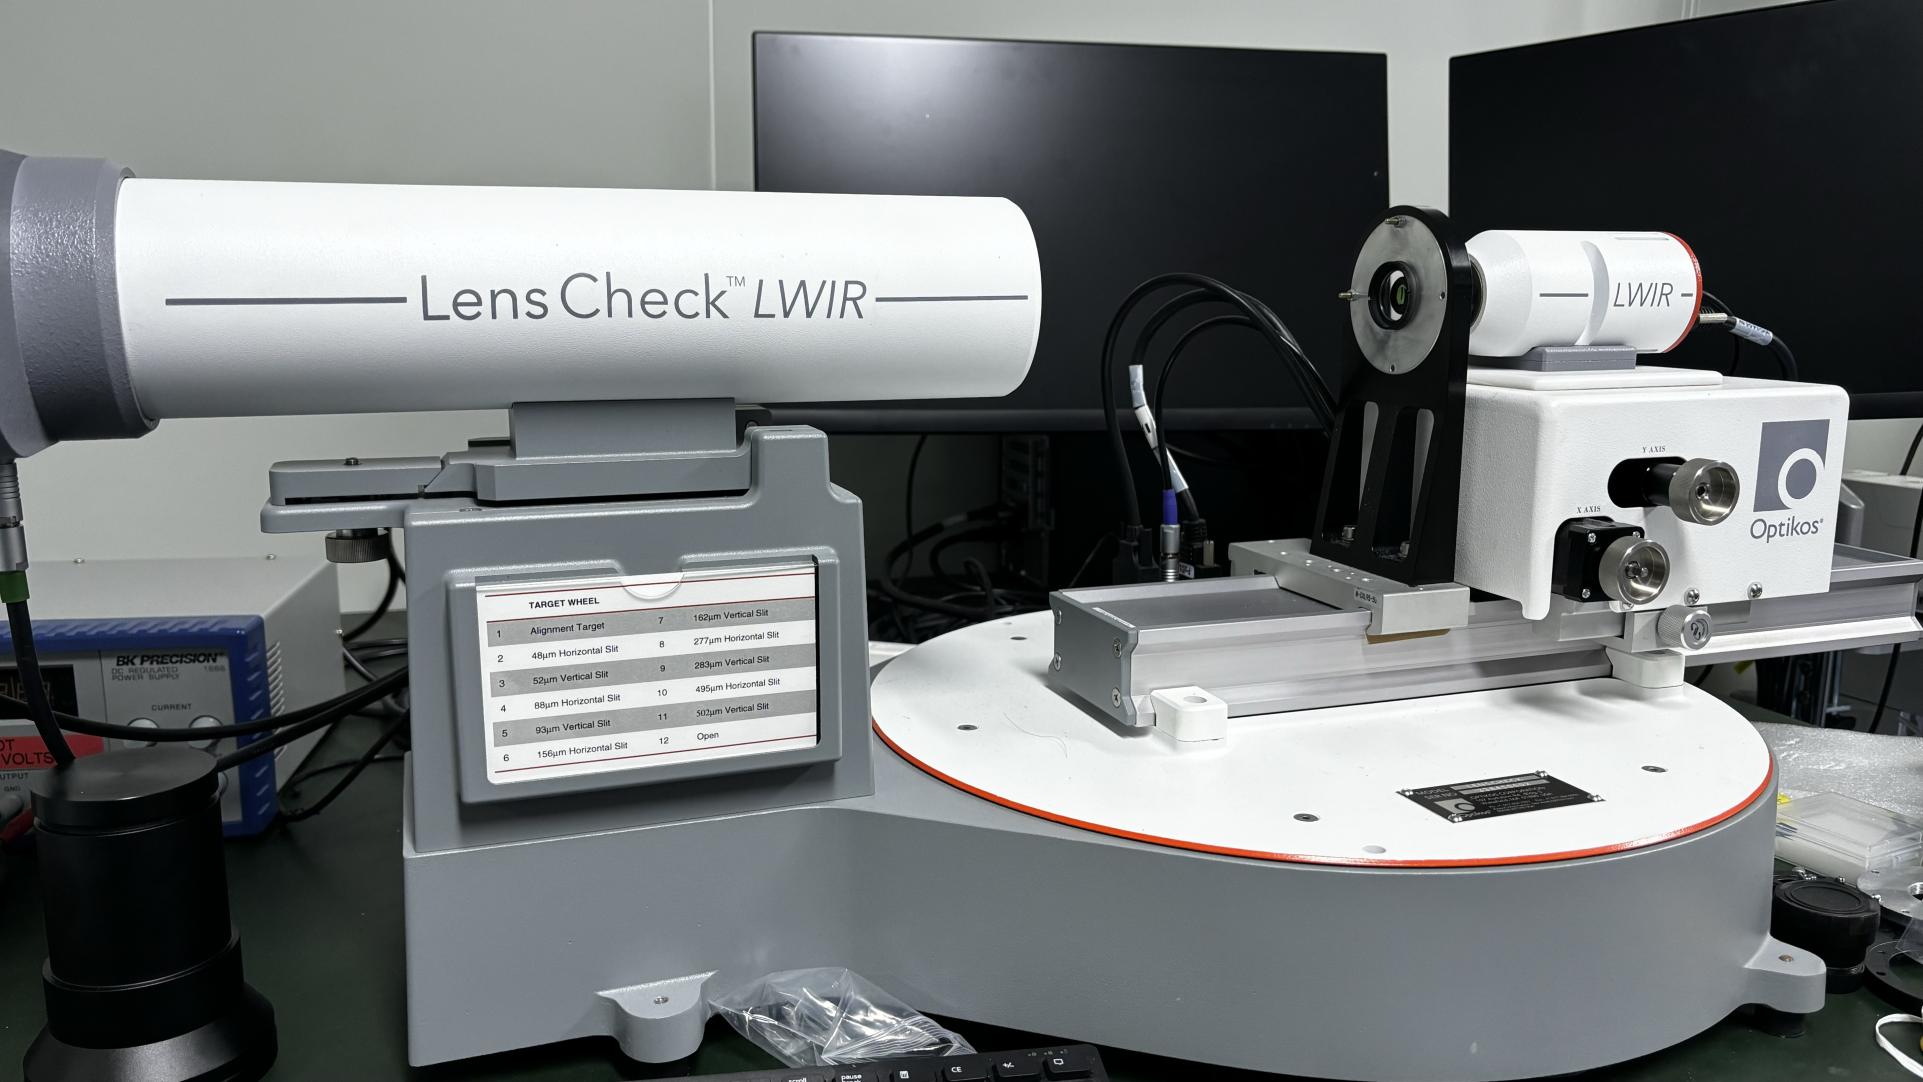
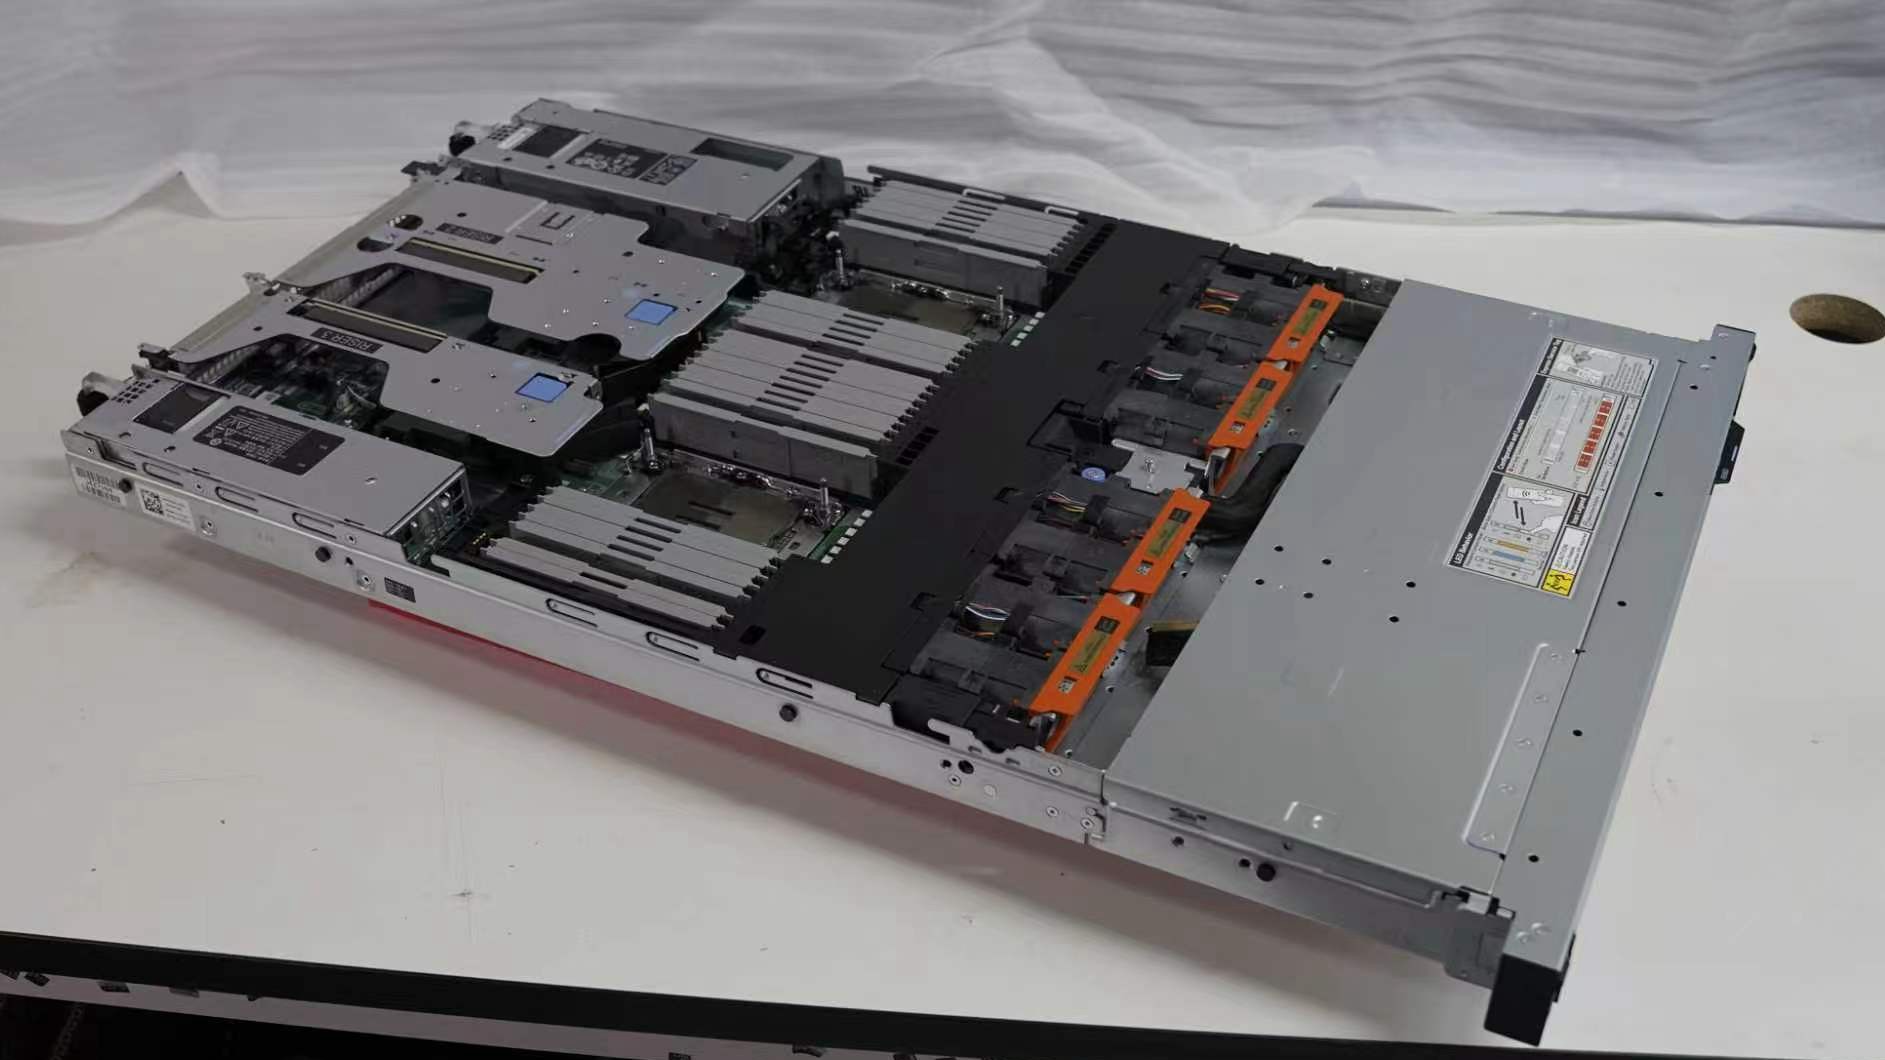
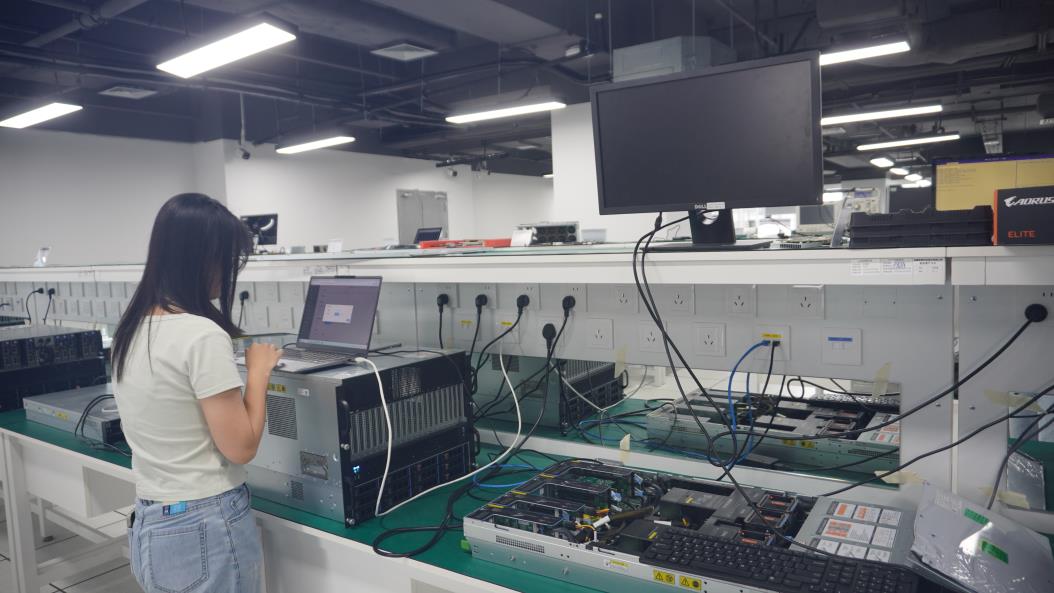
Understanding how technical specifications align with real-world enterprise deployment environments.
High-density office environments require seamless integration between SIP trunking, PoE switches, and high-performance structured cabling. Our connectors and optical modules ensure zero packet loss during peak operational hours.
Customer service operations demand crystal-clear audio transmission, low jitter, and uninterrupted uptime. Reliable transformer modules and robust transceivers prevent acoustic dropouts and maintain secure server connections.
Mission-critical medical communications require encrypted VoIP transmission and compliant hardware infrastructure. Our strict QC standards and robust manufacturing guarantee dependable performance in vital healthcare networks.
Browse additional high-reliability components engineered for comprehensive enterprise network architectures.
Expert answers regarding global procurement, manufacturing standards, and technical compatibility.
Buyers should evaluate manufacturing experience, international compliance certifications (CE, FCC, RoHS), supply chain stability, custom firmware capabilities, and responsive technical support to ensure seamless long-term deployment.
We implement a dual-layer quality assurance system featuring 100% automated optical testing, manual inspection by certified QC professionals, and rigorous environmental stress screening before shipment.
Yes. With an R&D team of 85+ engineers and over 120 new product releases annually, we offer comprehensive OEM/ODM customization covering custom wavelengths, transmission distances, packaging, and protocol compatibility.
Thanks to our robust upstream and downstream supply network comprising over 1,200 strategic partners, we maintain high component availability and ensure fast production scalability to meet tight delivery deadlines.